CNC PROBING · Accuracy starts at the machine Log in / Sign up
TR RU 中文
CNC PROBING

On-machine measurement and tool control systems

We do not take the part off the machine to measure it.

Measure your workpiece on your CNC machine

Taking a part off the machine to measure it and waiting in line at the inspection room is one of the most expensive habits in manufacturing. Once the part comes off, the set-up reference is lost; even when an error is found, the part has to be re-clamped and re-datumed to correct it. Measuring on the machine removes this loop.

An interface that is easy to use

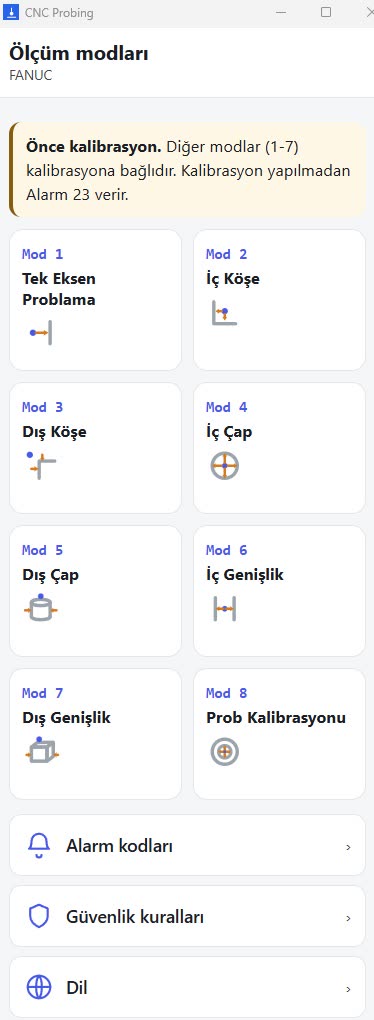
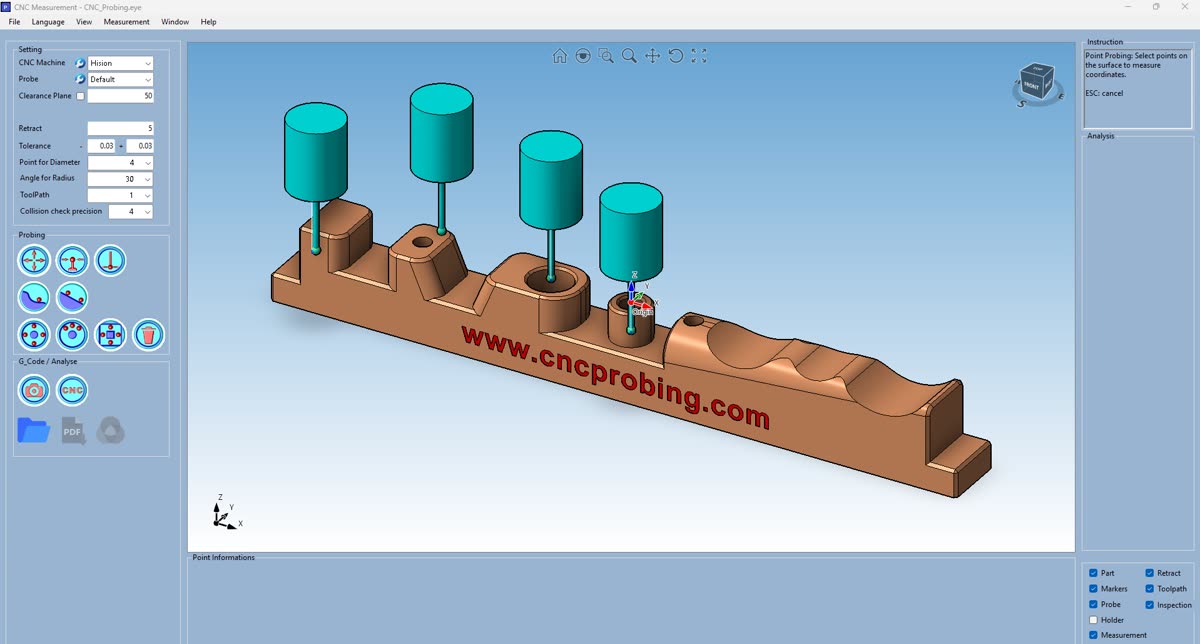
Measurement types sit as icons in the left panel and the part appears in the centre of the screen in 3D. Tolerance, retract distance, the number of points for a diameter and the collision check precision are gathered in one place on the same screen. A measurement point is picked on the part itself and the chosen point is marked on screen straight away. The user works while seeing what is being done.

CNC machine library

The software keeps its own machine library. Every machine tool in the shop is defined as a separate record, edited, and set as the active machine when needed. A separate macro is produced for each machine, so records do not get mixed up in a shop running several machines.

The software resolves macro conflicts

Macros are already stored in the machine control. If a macro added from outside uses the same number, a conflict arises. CNC Probing does not leave this to the user: it analyses the macros found on the machine and produces a macro specific to that machine which does not clash with the existing ones. The process is automatic. There is no macro number to choose, no macro to write, and no technical staff to call in for it.

Probe library and instant 3D

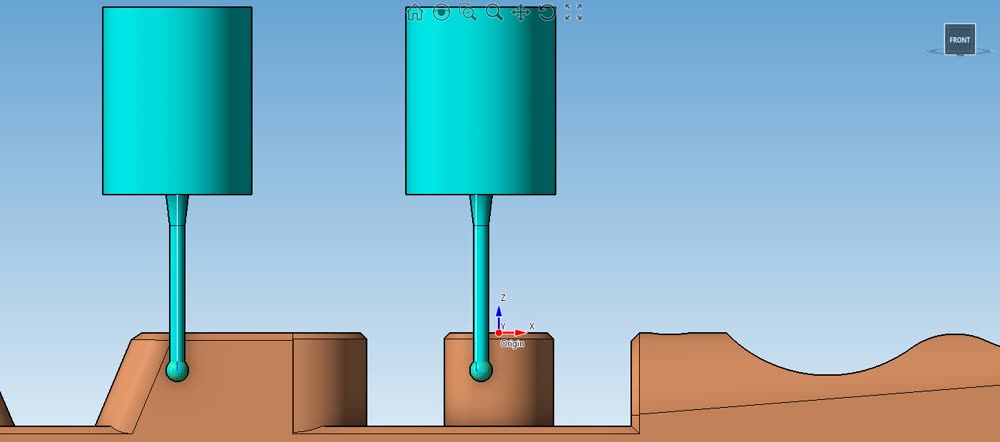
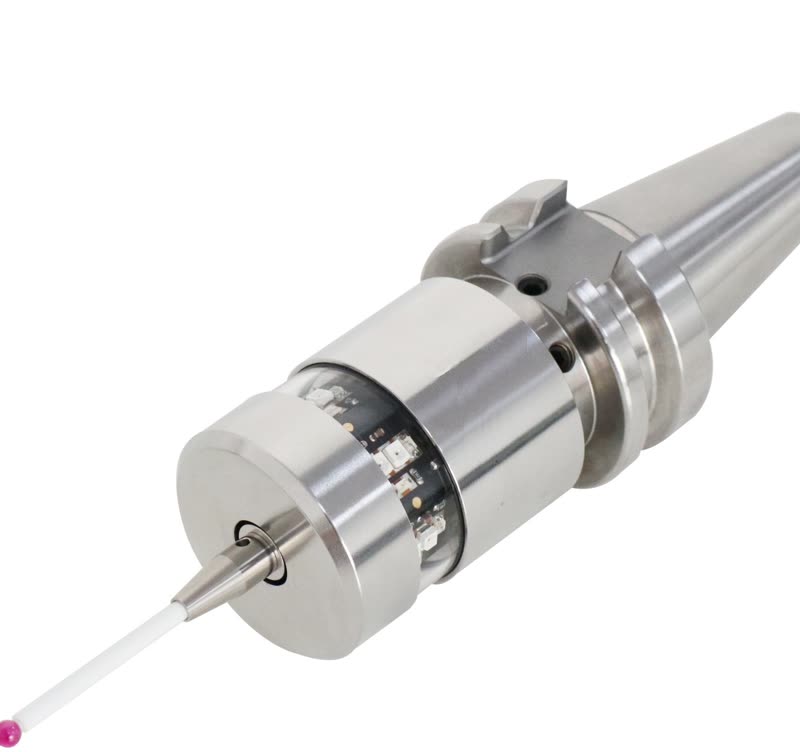
Probes are kept in a library as well. You can select a stored probe or define your own: stylus diameter, stem diameter, body diameter, lengths and holder dimensions are entered. As the values are entered, the probe and the holder are built on screen in 3D at the same time, with a dimensioned diagram beside them.

Case study

400,000 euro a year in a twenty-machine shop

What happens when measurement moves into the machine

A mid-sized manufacturer producing spare parts and moulds for a sector where a measurement record must be kept and traceable for every part runs twenty CNC machining centres. Their problem was not technical: the machines ran and the parts were in tolerance. The problem was how long the machines were not running.

In this sector the measurement record is as much a deliverable as the part itself.
400,000 €per year
20 CNC machining centrespayback: under one year

Before

At every new setup the operator found the datum by hand. Tool lengths were also set by hand, by the operator, at the machine. For inspection the part was unclamped and sent to the measuring room, and the machine waited for the result.

A broken tool was usually noticed at the end of the program; every part machined in that program then became suspect. When and why the machines stopped was not recorded at all.

What was done

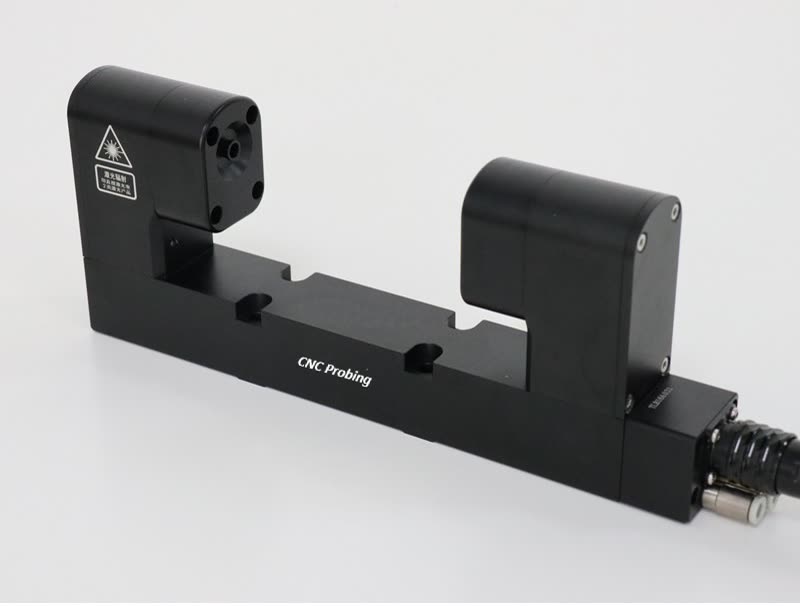
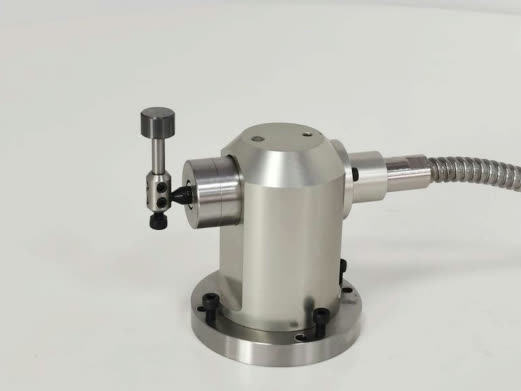
CNC Probing software, a measuring probe and a tool setter were installed on all twenty machines. CNC Control monitoring software was connected to the same machines. Installation took one macro per machine; the control units were not modified.

Result

Finding the datum went from about twenty minutes per setup to two. Tool length and diameter are now measured automatically on the machine instead of by hand.

Because the part is measured on the machine, the unclamp-reclamp cycle and the wait for the measuring room are gone. Broken tools are caught within the cycle; no bad part moves to the next operation.

Measurement results are reported in Q-DAS format as they are taken, so traceability is unbroken at part level. The investment paid for itself in less than a year, and the largest item was not scrap but machine downtime.

Annual saving — worked example

ItemCalculationPer year
Datum and tool setting time20 machines × 35 min/day × 250 days = 2,917 h175,000 €
Downtime for inspection and re-clamping20 machines × 15 min/day × 250 days = 1,250 h75,000 €
Reduction in scrap and reworkabout one third of the annual scrap cost90,000 €
Damage and suspect parts from broken toolsone incident a month instead of one a shift60,000 €
Total400,000 €

A machine hour rate of 60 euro has been used. The figures come from the company’s own records and vary from shop to shop. Recalculate with your own machine hour rate.

Before and after

DatumBy hand, ~20 min per setupWith the probe, ~2 min
Tool length and diameterSet by hand at the machineAutomatic, straight into the offset table
Part inspectionUnclamp, wait for the measuring roomOn the machine while clamped
Broken toolNoticed at the end of the programCaught within the cycle
Measurement recordCompiled by handAutomatic, in Q-DAS format
Reason for downtimeVerbally, at the end of the shiftLive, recorded, with alerts
“The machine used to stand idle at every new setup while the operator hunted for the datum. Now the probe finds it and we spend that time cutting. Across twenty machines that is hours a day.”
Production manager
“What I feared most was seeing a broken tool when the program ended. We would set every part from that program aside as suspect. Now the machine stops itself and we lose one part.”
Machine operator