
Machine monitoring software
CNC Control
Live machine monitoring and deviation alerts
What a machine produces is recorded. How long it does not produce usually is not. CNC Control closes that gap: it monitors the live state of the machine, reports a deviation the moment it happens, and transfers the program to the machine itself.
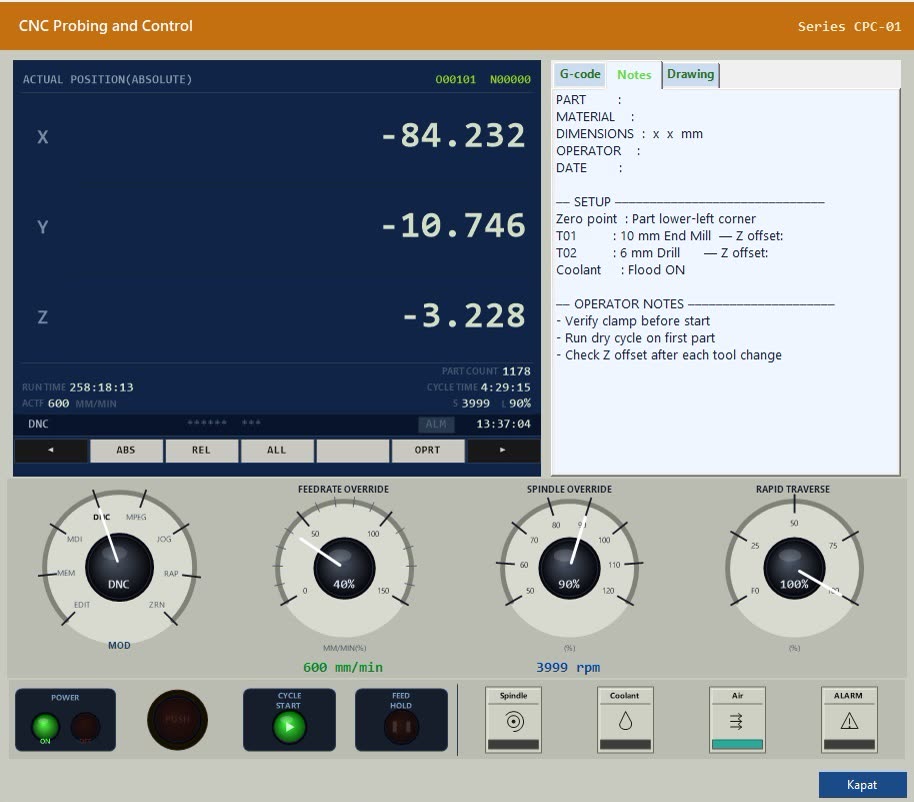
The whole machine on one screen
The software reads the state of the connected machines live. Axis positions, run time, cycle time, part count, feed and spindle override, the tool in use and the Gcode (tool path) line currently running are all on one screen. Setup information and operator notes are read from the same screen: part, material, datum, tool list and warnings are all on record.
It notices the deviation
The software does not only record. When there is an unusual stop, a drop in running speed or an unnecessary lengthening of the cycle time, it raises an alert. The alert goes to three levels at once: the operator at the machine, the production control supervisor and the management. The problem is seen when it happens, not at the end of the shift. The improvement measured in the field reaches twenty per cent on downtime reduction and cycle time conformance combined.
Program transfer over FTP
The program is sent to the machine directly from the computer. Carrying it by USB stick or CF card disappears. This is not only a time saving: loading the wrong version, copying a file incompletely and losing the card are common failures. When the transfer goes through the software, which program went to which machine and when is also recorded.
Drawing and solid model on the same screen
2D technical drawings and 3D solid models can be viewed inside the software. The operator opens the drawing of the part at the machine without leaving the program. Dimensions, clamping orientation and machining order are verified visually. No hunting for a paper drawing and no walk to the office.
The next job is prepared in advance
A list of the Gcode (tool path) programs that have run is kept. Which tools and which fixturing the next program will need is visible in advance, so tool and part preparation happens while the machine is still cutting. When the program ends the machine moves straight to the next job.
No modification to the control unit
The software reads data over the machine’s own communication interface. The control unit is not modified, the program is not changed and no extra hardware is needed. Control units in common use across the industry are supported.
Where the money comes from
Most of the saving comes not from scrap but from the time the machine is not cutting. The hourly cost of a machining centre is often higher than the material cost of the part made in that hour, so every minute of downtime is a direct cost.
Where programs are transferred by hand the machine waits at every program change, and loading the wrong version means scrap. If the next job is not prepared while the machine runs, it stops again the moment the program ends.
The slow lengthening of cycle time is the most insidious item. Nobody notices it because the machine appears to be running, yet the same part takes a little longer each time. CNC Control measures that drift, so the loss is stopped before it grows.
Run and cycle time: Run time, cycle time, part count
Feed and spindle: Feed override, spindle speed, rapid traverse
Tool and part: Tool in use, part being machined, parameters
Gcode (tool path): Running program line and program list
Downtime: Duration and reason for the stop
Alarm: Alarm state from the control unit
Setup and notes: Datum, tool list, operator warnings
Production control supervisor: within the shift
Management: daily summary
Waiting for program transfer
Scrap from loading the wrong program
Waiting for tool and fixture preparation
Unnoticed lengthening of cycle time
Leaving the machine to find a drawing
Manual reporting at the end of the shift
On the investment side there is no extra hardware: the software uses the existing communication interface of the machines.
CNC Probing gives the result of the measurement: is the part in tolerance, is the tool worn. CNC Control gives the flow of production: is the machine running, how fast, why did it stop. Used together, the record of both the part and the machine is unbroken.